
Custom Machining Parts Cost in 2026: A Buyer's Cost Model Led by Material Selection
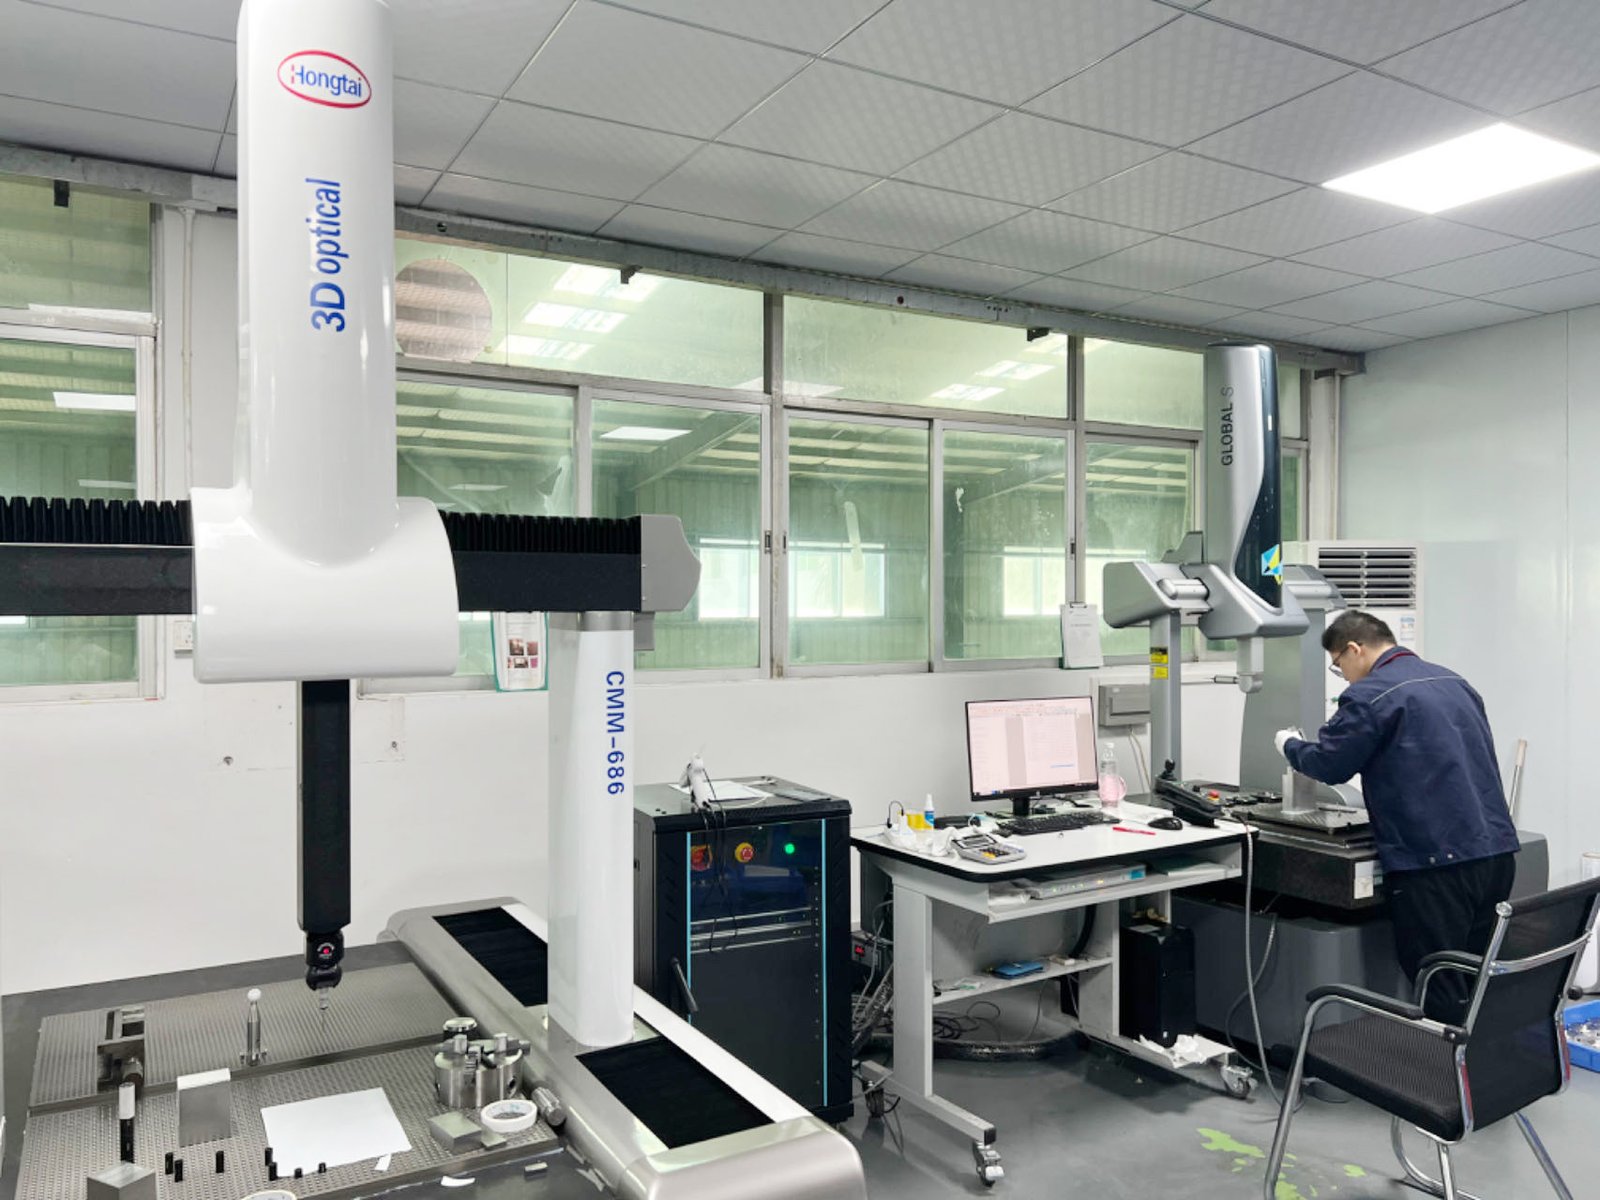
Custom machined parts are usually quoted after the material is chosen, but they are priced by that choice. The material decides the cycle time, the tool wear, the finishing path, and in many cases the lead time, before the shop ever touches the drawing. Aluminum cuts fast and holds size; stainless justifies a higher cost and a longer lead where corrosion demands it; titanium is worth the difficulty only where weight and strength both matter. Choose the material for the function, and the cost model mostly writes itself — choose it for the machinability, and you pay for the part twice. This guide is the buyer's cost model for custom machining parts in 2026: the line items behind the price, how the material families stack up on cost and lead time, how tolerance, finish, and quantity move each line, what a material-led quote should itemize, and a three-step method for building a budget you can defend to engineering and finance alike.
What does a custom machined part actually cost — line by line?
Every honest quote is the same five lines, with the material line at the top because it feeds every line below it. The material sets the stock cost, the cycle, the tooling, and the finish options, which is why the material conversation belongs at the start of the quote, not buried in a footnote.
| Line item | What it pays for | What moves it |
|---|---|---|
| Material stock | The bar, plate, or billet at the grade on the drawing | Grade, temper, and traceable certified lots |
| Machining time | Spindle minutes at the feed the material demands | Material machinability first, then features and tolerance |
| Setup and programming | Fixturing, toolpath work, first-piece prove-out | A one-time cost per order that dominates small quantities |
| Finishing and special processes | Anodizing, plating, heat treatment, and the rest | Metal-specific; the finish must be matched to the alloy |
| Inspection and documentation | CMM time, dimensional reports, material certificates | Each tight feature and GD&T category adds measurement and proof |
No honest shop quotes a price before the material is locked, because "custom machined parts" without a grade is not a specification — 6061-T6, 316L, and Ti-6Al-4V are three different parts with three different prices.
How do the material families stack up on cost and lead time?
Material moves the price twice: as stock and as machining time, and it moves the schedule the same way. Aluminum 6061 is the least expensive precision metal to machine — it cuts fast, holds the ±0.003 mm band predictably, and anodizes evenly, which makes it the default for housings and brackets where nothing in service demands more. Steel, in grades such as 4140 and 1045, earns its place when the part carries load or needs heat treatment, at a higher mill price and a longer lead. Stainless 303, 304, and 316 justifies a higher cost and longer lead time when corrosion resistance comes from the metal itself, with 303 the economical turned grade and 316 the choice for harsher environments. Brass and copper make sense for electrical and thermal work and machine freely. Titanium is worth the difficulty and the lead time only where weight and corrosion resistance both matter, because its premium is structural, not markup. Each of these comparisons is the subject of the material pages on this site; the cost model reads them in currency.
How much does the tolerance on the drawing move the price?
Machining cost is nonlinear in tolerance. Moving a feature from ±0.1 mm to ±0.003 mm can more than double the price, because the machine, the setups, the tooling, and the inspection method all change at once. Dropping a critical surface to ±0.002 mm moves it to grinding, a separate process family. On the floor behind this site, milling and turning hold ±0.003 mm on critical features and precision grinding reaches ±0.002 mm, with process capability tracked at Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window. And critical geometry verified on Hexagon CMMs. The material changes how hard the band is to hold across a run — a tough alloy holds size but costs more in cycle; a soft one cuts fast but needs controlled feeds — so the tolerance callout and the material callout belong on the same line of the cost model. Measurement scales with the band and the instrument: a general feature is checked with hand tools, a ±0.003 mm feature needs CMM time against your datum scheme, and a ground surface needs a roughness instrument. Ask what will be measured, with what instrument, and what the report will contain, and ask to see a sample CMM report from a completed job in the same material before you compare totals — the report is the only part of the tolerance you can audit after the parts ship. Reserve the tight band for the features that engage another part, leave the rest on the general block, and read the quote to see whether inspection is a line.
Which finishes should the budget assume, and what do they cost?
Finishing is metal-specific, and a finish matched to the alloy is cheaper and more reliable than one bolted on afterward. Anodizing belongs to aluminum, with standard Type II a different job from hard Type III anodize; passivation and electropolishing belong to stainless; plating and heat treatment have their own substrates and cycles. Every finish grows the dimension or changes the surface, so the allowance has to be machined in, and every finish adds a line and a few days to the schedule. Name the finish on the first quote, not the fifth revision, because a part reviewed with its finish is a part whose final size and price do not surprise you at delivery. On this floor the finishing is material-matched and bundled, which removes the handoff where a coating surprise usually lands; when a supplier outsources the step, ask who performs it and what documentation travels with it, because the handoff is part of the price either way. The factory behind this site runs 100+ machines across a 6,800 m² floor, which is the capacity that keeps a one-part prototype on the same schedule as a production program; confirm the floor behind the quote before you budget around its date.
How do quantity and program stage change the unit price?
The one-time lines — setup, programming, fixturing, first-article inspection — are fixed whether you order one part or a thousand, so a prototype carries them all on one piece. Minimum order here is one piece, with prototypes on the same machines and tolerances as production, so the prototype price is the honest anchor and the production tier shows the fixed lines spread thin. Lead time tracks the same process count and the material availability — roughly 3 days for simple parts, 7 days for standard parts, and up to 30 days for complex parts with many steps, heat treatment, or finishing. When the date and the price come from different process counts, the quote is describing two different parts. Between the prototype and the production run sits the bridge order, ten to fifty parts that exercise the material, the tooling, and the inspection loop before you commit volume; a supplier that quotes all three tiers is showing you the whole cost curve instead of its two ends. The revision loop belongs on the same page: every design or finish change triggers a new first-article check, and a supplier that prices the loop as its own line is showing you the real cost of iterating.
What should a material-led quote itemize so you can compare suppliers?
A quote you can compare states its assumptions about the material and everything downstream of it. Make sure each supplier shows the material grade and how the lot is verified, the tolerance and GD&T it will actually hold per feature, the process route for each feature, the finish and heat treatment included and who performs it, and the quantity tier with prototype and production separated. When a line is missing, assume the cost is hiding rather than absent: a quote that absorbs inspection into the margin is a quote you cannot compare, and a quote that does not name the finish behind the final size has not priced the part as it will be delivered. Ask to see a sample CMM report from a completed job in the same material family, and ask the supplier to walk you through what its material review flagged — the answer tells you whether the quote was built on a material conversation or on a guess.
How do you build a 2026 custom-parts budget you can defend?
Build the budget the way the shop would run the material conversation — function first, material second, quantity third.
- Choose the material for the function before you ask for a number. Decide what the part must do in service — carry load, resist corrosion, conduct, hold a temperature — and let that choose the family, then the grade. A budget built on an unlocked material is a budget built on a guess, because the grade sets the cycle, the finish, and the lead.
- Get the DFM review before you fix the number. Send the drawing and ask the supplier to flag the features that are tighter than the function needs, the geometry that fights the tool for that material, and the finish that will change the final size. Fix the drawing first; then budget the fixed drawing, not the first draft.
- Quote prototype, bridge, and production on the same page. One piece at MOQ 1, on the same machines and tolerances as production, anchors the fixed costs; the bridge prices the transition; the production tier shows where the fixed lines land at volume. Compare suppliers only when all quotes state the same material grade, tolerance scope, and finishing plan.
Keep the closing rule in front of you: the cheapest quote is rarely the cheapest part in service, because a material chosen for machinability instead of function fails at the cost of the application, not the cost of the machining. Choose the material for the function, and the 2026 budget you build will survive contact with the floor.
Frequently Asked Questions
How much do custom machined parts cost in 2026?
No honest shop quotes a price without a drawing and a material grade, because the price is set by the material family, the number of tight features, the process count, the finishing, and the quantity. A simple 6061 part at production quantity sits low; a titanium part with heat treatment and many tight callouts at prototype quantity sits far higher.
Why does the material choice affect the price more than anything else?
Because the material sets the cycle time, the tool wear, and the finish options before the first cut. Aluminum and the free-machining grades cut fast; tougher grades cut slower and wear tools; and each family has its own finishing path and lead-time profile.
What tolerance can custom machining hold?
Milling and turning hold ±0.003 mm on critical features; precision grinding reaches ±0.002 mm for sealing and seating surfaces, with process capability tracked at Ppk ≥ 1.67 initial under SPC and critical geometry verified on Hexagon CMMs.
What is the minimum order for a first part?
One piece. Prototypes run on the same machines and tolerances as production, with first-article inspection, so you can validate the design and the finish before committing volume.
What is your lead time, and does it affect the price?
Lead time tracks process count and material: roughly 3 days for simple parts, 7 days for standard parts, and up to 30 days for complex parts with many steps, heat treatment, or finishing. Price and lead time should come from the same process count; a quote that prices one and dates another should be questioned.
Which materials do you machine, and which is cheapest?
Aluminum 6061 and 7075, steel including 4140 and 1045, stainless 303, 304, 316, and 17-4PH, brass, copper, titanium, and engineering plastics. Aluminum 6061 and the free-machining grades are the least expensive to run; titanium and the heat-treated steels sit higher. Every lot is verified against its mill certificate before cutting.
Which certifications back the factory?
ISO 9001, IATF 16949 (product design excluded), and ISO 14001 under third-party surveillance, with certificate numbers you can check with the registrar. The legal entity behind the brand is Dongguan Zhuohang Ltd, founded in 2005, running 100+ machines across a 6,800 m² floor.
Want a quote priced after the material conversation?
Email the STEP or IGES model, the material grade, and the toleranced 2D drawing to [email protected] or call +86 13126536955. You will get a material-and-finish recommendation, a design-for-manufacturing review, and an itemized quote with the prototype and production tiers on the same page.